Structural Fitter and Welder Emiliano Zabala
Structural Fitter and Welder
[email protected] | (719) 555-0166 | Pueblo, United States
Profile
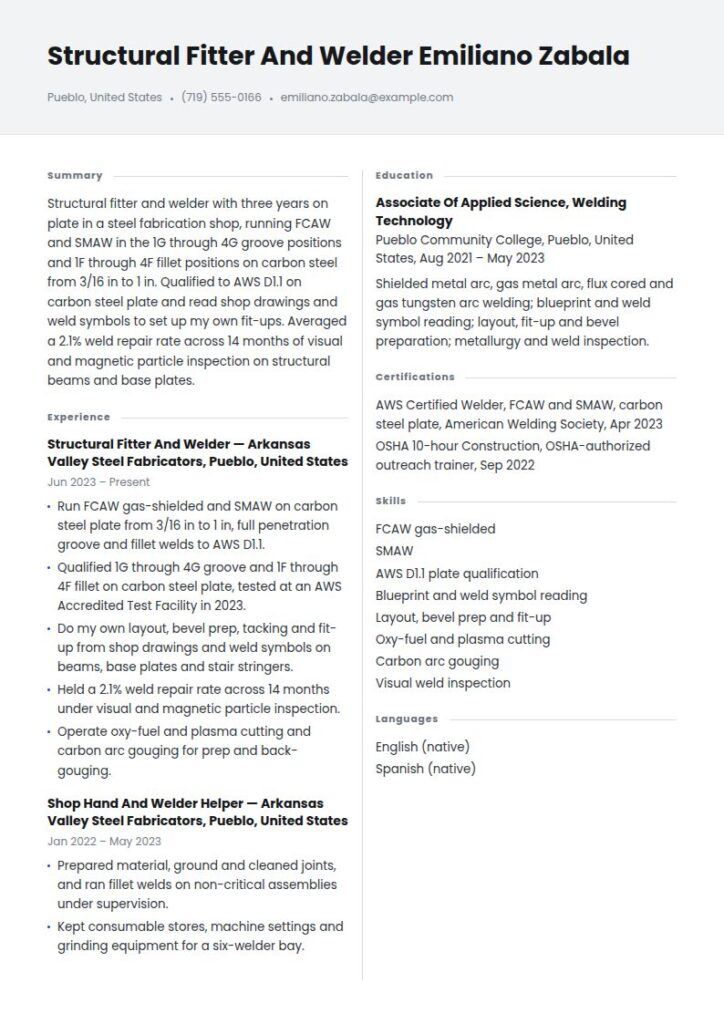
Structural fitter and welder with three years on plate in a steel fabrication shop, running FCAW and SMAW in the 1G through 4G groove positions and 1F through 4F fillet positions on carbon steel from 3/16 in to 1 in. Qualified to AWS D1.1 on carbon steel plate and read shop drawings and weld symbols to set up my own fit-ups. Averaged a 2.1% weld repair rate across 14 months of visual and magnetic particle inspection on structural beams and base plates.
Work Experience
06/2023 - Present, Structural Fitter and Welder, Arkansas Valley Steel Fabricators, Pueblo, United States
- Run FCAW gas-shielded and SMAW on carbon steel plate from 3/16 in to 1 in, full penetration groove and fillet welds to AWS D1.1.
- Qualified 1G through 4G groove and 1F through 4F fillet on carbon steel plate, tested at an AWS Accredited Test Facility in 2023.
- Do my own layout, bevel prep, tacking and fit-up from shop drawings and weld symbols on beams, base plates and stair stringers.
- Held a 2.1% weld repair rate across 14 months under visual and magnetic particle inspection.
- Operate oxy-fuel and plasma cutting and carbon arc gouging for prep and back-gouging.
01/2022 - 05/2023, Shop Hand and Welder Helper, Arkansas Valley Steel Fabricators, Pueblo, United States
- Prepared material, ground and cleaned joints, and ran fillet welds on non-critical assemblies under supervision.
- Kept consumable stores, machine settings and grinding equipment for a six-welder bay.
Education
08/2021 - 05/2023, Associate of Applied Science, Welding Technology, Pueblo Community College, Pueblo, United States
Shielded metal arc, gas metal arc, flux cored and gas tungsten arc welding; blueprint and weld symbol reading; layout, fit-up and bevel preparation; metallurgy and weld inspection.
Skills
FCAW gas-shielded, 85
SMAW, 80
AWS D1.1 plate qualification, 80
Blueprint and weld symbol reading, 75
Layout, bevel prep and fit-up, 75
Oxy-fuel and plasma cutting, 80
Carbon arc gouging, 70
Visual weld inspection, 70
Languages
English, native
Spanish, native
Certificates
04/2023, AWS Certified Welder, FCAW and SMAW, carbon steel plate, American Welding Society
Performance test at an AWS Accredited Test Facility judged by an AWS Certified Welding Inspector. Maintenance documentation submitted every six months and current.
09/2022, OSHA 10-hour Construction, OSHA-authorized outreach trainer
Summary
A welder resume is a one to two page document whose real content is the qualification record: the processes you run, the positions you are qualified in written in code letters, the base materials and thicknesses, the code you tested to, and whether that qualification is still current. This guide gives you three adaptable versions and current Bureau of Labor Statistics pay and outlook for the trade.
Welder resume examples by experience level
A welder resume is a one to two page document built around one thing: the qualification record. Processes, positions in code letters, base materials and thicknesses, the code you tested to, and the date that proves it is still live.
Nobody hires a welder in general. A shop hires against a specific welding procedure specification, and the only question in the foreman's head while he reads your file is whether you are already qualified to run it or whether he has to pay for a test to find out.
Resume guide for a welder resume
This guide and the corresponding welder resume example will cover:
- How to write a welder resume, section by section
- How to write your qualification record so a foreman can read it in four seconds
- Three adaptable summaries: structural fitter, pipe welder and weld shop foreman
- What the AWS Certified Welder credential is, and why continuity keeps it alive
- What the trade pays and where the work sits
How to write a welder resume
Five sections: contact header, summary, qualification record, work experience, and education with certifications. One page for your first ten years. Two once you run a shop, hold procedure documentation or train testers.
The qualification record goes directly under the summary, above experience. It is the only block a hiring foreman is guaranteed to read, and burying it inside job bullets is the single most common mistake on a welding resume.
| Section | What it is answering | Where it goes |
|---|---|---|
| Qualification record | Can this person run our WPS without a retest? | Directly under the summary |
| Work experience | What have they built, in what materials, to what code? | Reverse chronological |
| Fitting and layout | Can they set up work, or only burn rod? | Inside experience bullets |
| Certifications | Is the paperwork current? | With dates and the test facility |
Write the four variables in one line, not four paragraphs
A welding qualification has four variables: process, position, base material and thickness, and the code the test was run to. Put them on one line each and a foreman reads your whole scope in seconds.
"GTAW and SMAW, 6G, carbon steel and 316L stainless pipe, tested to ASME Section IX, current."
Compare with "experienced welder proficient in multiple welding processes with a strong safety record". The second version forces the foreman to schedule a test to find out what the first version already told him, which is why the first version gets called first.
Run the finished file through the free Rezoom ATS resume checker before you send it. Large fabricators and mechanical contractors run applications through a parser, and a qualification table in two columns is exactly what a parser scrambles.
Choosing the best resume format for a welder resume
Reverse chronological, with the qualification record hoisted to the top as its own block. That hybrid is standard in the trade and no foreman finds it odd.
Do not use a functional format. Welding hiring is suspicious of gaps for a specific reason: continuity of qualification. A format that hides when you were welding also hides whether you have been welding, and that is the question the format is being asked.
Include your contact information
| ✅ Right | ❌ Wrong |
|---|---|
| Emiliano Zabala | Emiliano Zabala |
| Pipe Welder, 6G, GTAW and SMAW, ASME Section IX | Hardworking welder with great work ethic |
| AWS Certified Welder, maintenance current to September 2026 | AWS certified |
| (719) 555-0166, [email protected], Pueblo, CO | (719) 555-0166, [email protected] |
The second line is doing more work than the rest of the page. Process, position, code. A foreman scanning twenty files is looking for exactly those three tokens and nothing else.
Make use of a summary
Four lines: your trade and years, the processes and positions, the materials and code, and one number about output or quality.
Structural fitter and welder with three years on plate in a steel fabrication shop, running FCAW and SMAW in the 1G through 4G groove positions and 1F through 4F fillet positions on carbon steel from 3/16 in to 1 in. Qualified to AWS D1.1 on carbon steel plate and read shop drawings and weld symbols to set up my own fit-ups. Averaged a 2.1% weld repair rate across 14 months of visual and magnetic particle inspection on structural beams and base plates.
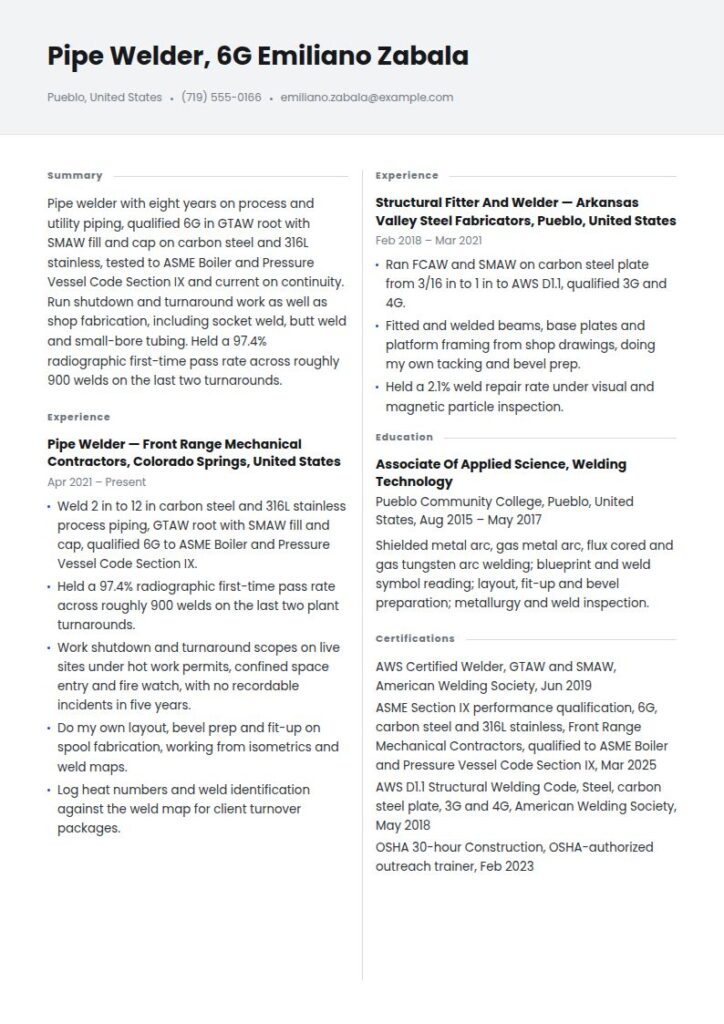
Pipe welder with eight years on process and utility piping, qualified 6G in GTAW root with SMAW fill and cap on carbon steel and 316L stainless, tested to ASME Boiler and Pressure Vessel Code Section IX and current on continuity. Run shutdown and turnaround work as well as shop fabrication, including socket weld, butt weld and small-bore tubing. Held a 97.4% radiographic first-time pass rate across roughly 900 welds on the last two turnarounds.
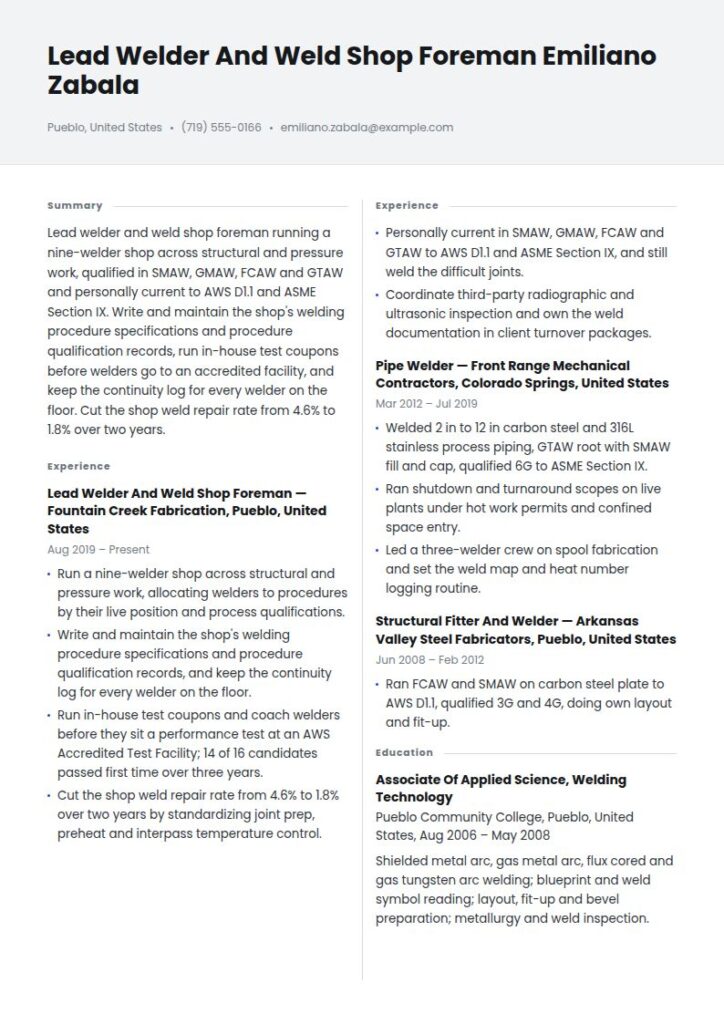
Lead welder and weld shop foreman running a nine-welder shop across structural and pressure work, qualified in SMAW, GMAW, FCAW and GTAW and personally current to AWS D1.1 and ASME Section IX. Write and maintain the shop's welding procedure specifications and procedure qualification records, run in-house test coupons before welders go to an accredited facility, and keep the continuity log for every welder on the floor. Cut the shop weld repair rate from 4.6% to 1.8% over two years.
Right vs wrong: the same welder summary, twice
| ✅ Right | ❌ Wrong |
|---|---|
| Pipe welder, eight years, 6G GTAW root with SMAW fill and cap, carbon steel and 316L stainless. | Experienced welder skilled in multiple welding processes. |
| Tested to ASME Boiler and Pressure Vessel Code Section IX and current on continuity. | Certified welder with all necessary certifications. |
| 97.4% radiographic first-time pass rate across roughly 900 welds on the last two turnarounds. | Committed to quality workmanship and safety. |
The right column can be put on a joint on Monday. The left column has to be tested first, and testing costs the shop money before you have made it any.
Outline your welding experience
Employer, what the shop builds, and dates. Then three to five bullets naming the process, the material, the joint type and a number.
| Instead of | Use |
|---|---|
| Welded various metals using different processes | Ran FCAW on carbon steel plate from 1/4 in to 1 in, full penetration groove welds to AWS D1.1 |
| Responsible for high quality welds | Held a 2.1% weld repair rate over 14 months across visual and magnetic particle inspection |
| Read blueprints | Worked from fabrication drawings and weld symbols, doing my own fit-up, tacking and bevel prep |
| Worked on pipe | Welded 2 in to 12 in carbon steel and 316L stainless process piping, GTAW root with SMAW fill and cap |
| Followed safety procedures | Ran hot work permits, confined space entry and fire watch on live-plant turnaround work |
Pipe Welder, Front Range Mechanical Contractors, Colorado Springs, CO, April 2021 to Present. Process and utility piping for food, chemical and municipal water clients.
Weld 2 in to 12 in carbon steel and 316L stainless process piping, GTAW root with SMAW fill and cap, qualified 6G to ASME Section IX.
Held a 97.4% radiographic first-time pass rate across roughly 900 welds on the last two plant turnarounds.
Work shutdowns and turnarounds on live sites, including hot work permits, confined space entry and fire watch, with no recordable incidents in five years.
Do my own layout, bevel prep and fit-up on spool fabrication, working from isometrics and weld maps.
Log every heat number and weld identification against the weld map for the client's turnover package.
Process, position and procedure: your qualification record is the resume
Every other section is context. This is the section a foreman reads.
A welder is not hired as a welder. A welder is hired against a welding procedure specification, a WPS, which fixes the process, the base metal and thickness range, the filler, the position, the joint design, the preheat and the electrical parameters. Your qualification either falls inside that procedure or it does not. So write your record in the same vocabulary the procedure uses.
Processes, in their code letters. SMAW for stick, GMAW for MIG including short circuit and spray transfer, FCAW self-shielded or gas-shielded, GTAW for TIG. Write the abbreviation and the common name together the first time, then use the abbreviation. Naming four processes when you are genuinely fluent in two is a mistake, because the test will find out.
Positions, in code. Groove welds run 1G flat, 2G horizontal, 3G vertical, 4G overhead, plus 5G and 6G on fixed pipe. Fillet welds run 1F through 4F. Say plate or pipe, because they are not the same test. 6G is the one most pipe shops test on: the pipe is fixed at a 45 degree angle and cannot be rotated, so it puts every position into a single weld.
Base materials and thicknesses. Carbon steel, stainless by grade, aluminum by alloy, chrome-moly, duplex. Give the thickness range on plate and the diameter and schedule range on pipe. A shop that runs thin-wall stainless tube has a different problem from one running 1 in structural plate, and both need to see the number.
The code you tested to. AWS D1.1 Structural Welding Code, Steel, is the usual structural test. ASME Boiler and Pressure Vessel Code Section IX governs procedure and performance qualification on pressure work. Name the code, name the test facility, and give the date.
Processes: GTAW, SMAW, FCAW gas-shielded, GMAW short circuit and spray
Positions: 6G and 5G on pipe; 1G through 4G groove and 1F through 4F fillet on plate
Materials: carbon steel; 304 and 316L stainless; pipe 1/2 in to 12 in, schedule 10 through schedule 80; plate 3/16 in to 1 in
Codes: ASME Boiler and Pressure Vessel Code Section IX, performance qualification, current. AWS D1.1 Structural Welding Code, Steel, carbon steel plate.
AWS Certified Welder: tested at an AWS Accredited Test Facility, maintenance documentation submitted and current to September 2026.
Inspection experience: radiographic, ultrasonic, magnetic particle and dye penetrant testing on my own work; weld map and heat number logging for turnover packages.
Then the part almost nobody writes down, and the part that makes the whole block worth something.
A lapsed continuity record turns a certification line into decoration
The AWS Certified Welder program is strictly performance-based. There is no prerequisite course. You take a hands-on test at an AWS Accredited Test Facility, and the test is judged by an AWS Certified Welding Inspector. Testing follows the AWS QC47 specification and AWS Standard Welding Procedure Specifications, and some facilities will test you to an employer's own procedure instead (American Welding Society program page, read 12 September 2026).
The part that catches people out is what happens afterwards. AWS states that to keep the certification active, the welder must submit certification maintenance documentation every six months confirming that they continue to perform the process for which they were certified (AWS, September 2026).
So a resume line reading "AWS Certified Welder, 2019" is worth almost nothing on its own. A hiring foreman reads it and immediately wonders whether the maintenance has been filed since. Write the currency instead: "AWS Certified Welder, GTAW and SMAW, maintenance documentation current to September 2026." One clause, and the question is closed.
The same logic applies to employer and code qualifications. If you have been off a process for a long stretch, say what you have been doing and say you are ready to retest. Foremen respect that answer. They do not respect finding out on the test coupon.
And the negative case, which is worth stating plainly. "Certified welder" with no process, no position and no code named tells a shop nothing at all. It cannot be matched to a procedure, it cannot be verified, and the reader has to assume the least favorable interpretation, because the applicants who could name their scope did.
Build a snapshot of your key skills
Ten to fourteen entries in three groups: processes and equipment, fabrication skills, and site skills.
Processes and equipment: GTAW, SMAW, FCAW, GMAW, oxy-fuel and plasma cutting, carbon arc gouging, orbital tube welding, inverter and engine-driven machines
Fabrication: Blueprint and isometric reading, weld symbols, layout and bevel prep, fit-up and tacking, pipe fitting, grinding and finishing, preheat and interpass temperature control
Quality and inspection: Visual inspection, weld map and heat number logging, working alongside radiographic, ultrasonic, magnetic particle and dye penetrant testing, WPS and PQR documentation
Site: Hot work permits, confined space entry, fire watch, rigging and signaling, aerial lift, turnaround and shutdown work
List your education and certifications
Certifications with dates and the testing facility, then the trade program, then the safety cards.
AWS Certified Welder, American Welding Society, tested at an AWS Accredited Test Facility, GTAW and SMAW; maintenance documentation current to September 2026
ASME Boiler and Pressure Vessel Code Section IX performance qualification, 6G, carbon steel and 316L stainless, employer-held, requalified 2025
AWS D1.1 Structural Welding Code, Steel, carbon steel plate, 3G and 4G, 2018
Associate of Applied Science, Welding Technology, Pueblo Community College, Pueblo, CO, 2017
OSHA 30-hour Construction, 2023. Confined space entry and rescue awareness, 2024. First aid and CPR, 2025.
Choose the right layout and design
Single column, 11 or 12 point, no photograph, no graphics, no skill bars. Put the qualification record in plain labeled lines rather than a table, because that is the block you cannot afford to lose to a parser.
Write processes in their code letters and positions in their code numbers. Say plate or pipe. Give material grades, thickness and diameter ranges. Name the code you tested to and the date. State the currency of your AWS maintenance documentation. Say whether you do your own fit-up and bevel prep. Give a repair rate or a radiographic pass rate if you have one.
Do not write "certified welder" with nothing after it. Do not list a process you cannot pass a test on today. Do not hide dates, because continuity is exactly what the reader is checking. Do not put your qualification record in a two-column table on a file going through a portal. Do not claim a code qualification that was held by a previous employer without saying so.
Welder job market and outlook
A large trade with slow growth and steady replacement demand, concentrated in manufacturing but paid best outside it.
| Measure | Value |
|---|---|
| Welder, cutter, solderer and brazer jobs, 2025 | 437,700 |
| Projected jobs, 2035 | 448,100 |
| Projected change, 2025 to 2035 | 2% (slower than average), +10,300 |
| Projected annual openings | ~40,300 |
| Typical entry-level education | High school diploma or equivalent |
| Median annual wage, May 2025 | $53,750 ($25.84 per hour) |
Source: U.S. Bureau of Labor Statistics, Occupational Outlook Handbook, 2025-35 projections and May 2025 wage data.
Most welders work in manufacturing; the best paid ones do not
Manufacturing employs 63 percent of welders, cutters, solderers and brazers. Specialty trade contractors account for 8 percent, self-employed welders 4 percent, and repair and maintenance 4 percent (BLS Occupational Outlook Handbook, May 2025).
The pay ranking is close to inverted. Specialty trade contractors pay a median of $59,440, repair and maintenance $56,080, and manufacturing $51,210 (BLS, May 2025).
That is a gap of $8,230 a year between the largest employer of welders and the best paying one. The work in the higher band is field and contract work: mechanical piping, structural erection, plant maintenance and turnarounds, and it is gated almost entirely by position and code qualification rather than by years served. A shop welder with 3G plate qualification and a pipe welder with a current 6G ticket are in different markets, and moving between them is a test, not a promotion.
What salary you can expect as a welder
The median annual wage for welders, cutters, solderers and brazers was $53,750, or $25.84 an hour, as of May 2025. The lowest 10 percent earned less than $39,240 and the highest 10 percent more than $77,530 (BLS, May 2025).
For comparison, the whole production occupations group had a median annual wage of $46,990 in May 2025, so welding sits meaningfully above the average production job (BLS Occupational Outlook Handbook, May 2025).
Three things move a welder up that range: the position and code you are qualified in, whether you can fit up your own work, and whether you will travel for shutdown and turnaround work. All three are things a resume can prove in one block. None of them is a personality trait, which is why the qualification record earns its place at the top of the page.
Key takeaways for a welder resume
- Put the qualification record directly under the summary, above experience.
- Name processes in code letters and positions in code numbers, and say plate or pipe.
- Give base materials by grade, plus thickness on plate and diameter and schedule on pipe.
- Name the code you tested to: AWS D1.1, ASME Section IX, or an employer procedure.
- State the currency of your AWS maintenance documentation, not just the year you tested.
- Say whether you do your own layout, bevel prep and fit-up.
- Give one quality number: repair rate, radiographic pass rate, or rejects per weld count.
Build your welder resume in 15 minutes.
Related production resume examples
- Machinist resume
- Manufacturing technician resume
- Machine operator resume
- Quality assurance resume
- Assembler resume
- Production worker resume
- Factory worker resume
- Material handler resume
- Forklift operator resume
- Production resume
- Operations manager resume
- Operations director resume
Pair it with a matching welder cover letter.
Welder resume questions, answered
How long should a welder resume be?
One page for your first ten years. Two once you run a shop, maintain welding procedure specifications, or hold a long list of live qualifications that genuinely needs the room. The qualification record is worth the space. A career objective is not.
What does AWS Certified Welder actually mean?
It is a performance-based credential: no prerequisite course, a hands-on test at an AWS Accredited Test Facility, judged by an AWS Certified Welding Inspector, following the AWS QC47 specification and AWS Standard Welding Procedure Specifications, or an employer's own procedure at some facilities. To keep it active, AWS requires certification maintenance documentation every six months confirming continued use of the process (American Welding Society, read 12 September 2026).
My qualification lapsed. Do I still list it?
Yes, with the honest date and a sentence about retesting. "ASME Section IX 6G, last qualified 2023, available to retest on request" is a normal, respected line in this trade. Leaving the date off so it reads as current is the version that ends badly, because the test coupon settles it in an afternoon.
Do I need to say which positions I am qualified in?
Yes, and in code. 3G plate and 6G pipe are different jobs at different rates. A foreman matching your file to a procedure needs the position codes to do it at all, and a resume that omits them puts the burden of finding out onto the person deciding whether to call you.
Is shop welding or field welding better paid?
Field and contract work generally pays more. Specialty trade contractors paid a median of $59,440 in May 2025 against $51,210 in manufacturing, though manufacturing employs 63 percent of the trade (BLS Occupational Outlook Handbook, May 2025). Field work also asks for travel, shutdown hours and a broader position qualification, which is what the difference is buying.